 EN
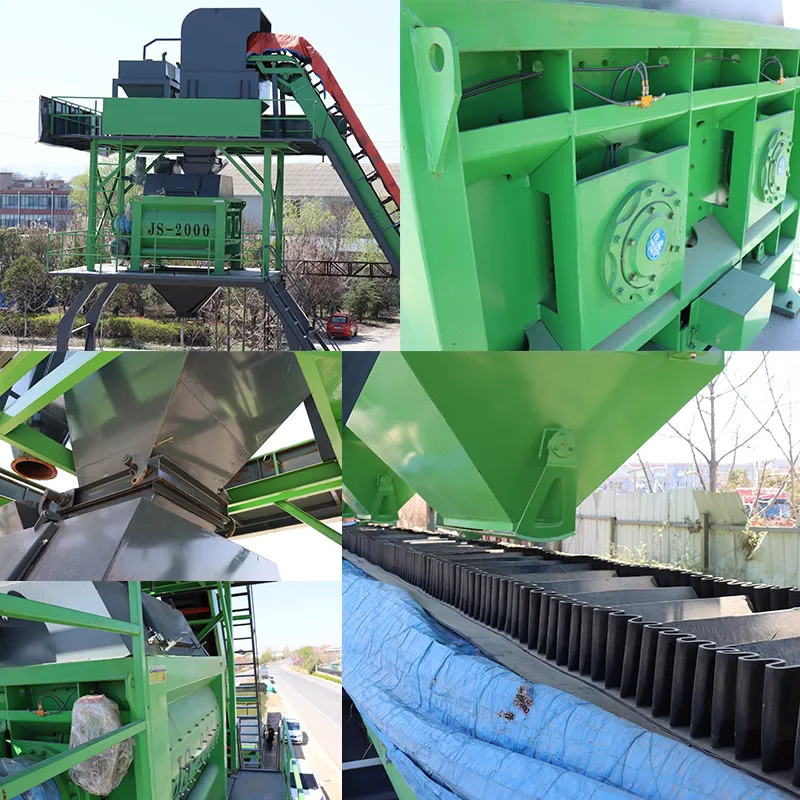
Modern industrial construction demands efficiency, precision, and scalability. A concrete mixer plant equipped with automation systems represents a significant advancement in ready mix concrete production. These systems integrate digital controls, real-time monitoring, and automated workflows to reduce manual intervention, improve batch consistency, and accelerate production cycles. For contractors, concrete producers, and infrastructure developers, understanding how automation transforms concrete batch plant capacity is essential for making informed equipment investments.
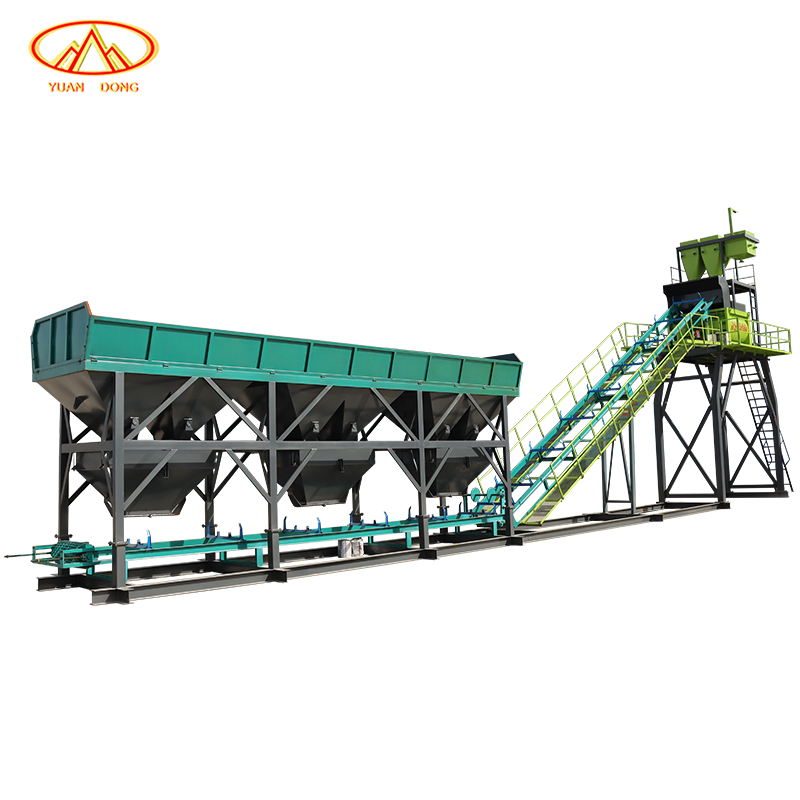
Automation in ready mix concrete production has fundamentally changed how batching plants operate. Rather than relying on manual mixing timers and operator judgment, modern systems use programmable logic controllers (PLCs) and sensor networks to manage every stage of production. This technological shift directly impacts mobile concrete mixer specifications, allowing operators to achieve tighter tolerances on water content, aggregate ratios, and admixture dosing. The result is more reliable concrete quality and higher throughput without sacrificing consistency.
Core Automation Technologies in Concrete Batch Plants
PLC-Controlled Batch Management
Programmable logic controllers form the backbone of modern concrete batch plant capacity management. These controllers receive input from load cells, flowmeters, and temperature sensors to automatically dispense materials in precise quantities. When a batch recipe is entered, the PLC system manages cement, aggregate, water, and admixtures in real-time, adjusting for material density variations and environmental conditions. This eliminates human error and ensures every batch meets specification, which is critical for ready mix concrete production where consistency is non-negotiable.
The automation also enables rapid recipe switching. Operators can store multiple concrete mixes in the system database and activate the correct formulation with a single command. Mobile concrete mixer specifications can be modified on-the-fly to match site requirements without equipment recalibration. For high-volume operations, this flexibility translates directly to increased concrete batch plant capacity and reduced downtime between job changes.
Sensor Integration and Real-Time Monitoring
Modern concrete mixer plant systems employ multiple sensors to track production parameters continuously. Load cells measure material weight during discharge, moisture sensors verify aggregate water content, and temperature probes ensure water temperature remains within acceptable ranges. These inputs feed into the control system, which makes micro-adjustments to maintain batch precision. If a sensor detects deviation from target values, the system can pause discharge or trigger alerts for operator review.
This real-time monitoring capability improves both ready mix concrete production quality and safety. Early detection of equipment issues—such as worn mixer blades or clogged pipes—prevents defects before they reach the customer. For concrete batch plant capacity planning, this means fewer rejected batches and less rework, directly improving overall output efficiency and profitability.
Impact of Automation on Production Efficiency
Increased Batch Cycle Speed
Automation accelerates the concrete batch plant capacity by reducing cycle time. Manual batching requires operators to visually confirm material levels, measure quantities, and monitor mixing duration. Automated systems eliminate these steps. Material dispensing begins the moment a batch is triggered, and the mixer discharge time is optimized based on mix design rather than operator experience. For a concrete mixer plant running 16-hour shifts, this time savings compound significantly across hundreds of batches.
The precise control also reduces over-mixing, which can weaken concrete and waste energy. Ready mix concrete production benefits from consistent mixing times calibrated to aggregate size and binder type. Mobile concrete mixer specifications define optimal mixing durations, and automation ensures these specifications are met without deviation, eliminating the risk of operator drift.
Reduced Material Waste and Cost Control
Overages and underages in material dispensing directly impact production cost. Manual batching often results in 2–5% material waste due to estimation errors or overfilling. Automation reduces this waste to under 1% because load cells confirm exact quantities before discharge. Over a year, this precision generates substantial cost savings for ready mix concrete production operations. Additionally, fewer rejected batches mean less concrete batch plant capacity lost to rework.
Labor cost reduction is another significant advantage. Fewer operators are needed to oversee a fully automated concrete mixer plant. A single supervisor can monitor multiple mixing stations, track data logs, and manage production schedules from a central control room. This is especially valuable for mobile concrete mixer specifications used on large infrastructure projects where labor costs are a major budget line item.
Scalability and Capacity Enhancement
Modular System Design
Modern automation platforms support modular expansion. A concrete batch plant capacity can be increased by adding mixer units or aggregate silos without replacing the entire control system. The PLC architecture accommodates new equipment, and sensor networks scale proportionally. This means initial investment in a concrete mixer plant automation system creates a platform for future growth.
Ready mix concrete production companies can start with a single-mixer setup and expand to multi-mixer facilities as demand grows. Each unit operates independently or in parallel, coordinated by the central controller. Mobile concrete mixer specifications remain consistent across all units, ensuring quality uniformity whether one mixer or ten are running. This scalability is essential for businesses planning long-term expansion without repeated equipment overhauls.
Data Analytics and Optimization
Automation systems generate detailed production data: batch times, material usage, equipment performance, and reject rates. Operators and managers can analyze these metrics to identify bottlenecks and optimize workflows. If concrete batch plant capacity analysis reveals that one mixer consistently runs slower than others, technicians can investigate and address root causes. This continuous improvement cycle directly boosts overall ready mix concrete production efficiency.
Data also supports mobile concrete mixer specifications adjustments. If field testing shows that a particular mix design can use slightly higher water content without compromising strength, the control system can be updated across all batches. This minor optimization, replicated across thousands of batches annually, yields measurable performance and cost gains.
FAQ
What is the primary benefit of automation in concrete batch plant operations?
The primary benefit is consistency and efficiency. Automation ensures every batch of ready mix concrete production meets exact specifications while reducing cycle time and material waste. A concrete mixer plant equipped with automation delivers higher concrete batch plant capacity per hour, fewer defects, and lower operating costs compared to manual batching.
How does automation improve mobile concrete mixer specifications compliance?
Automation enforces mix design specifications by controlling material proportions precisely. Sensors confirm that water content, aggregate ratios, and admixture dosages match the recipe before mixing begins. This ensures mobile concrete mixer specifications are met consistently, regardless of operator skill level or environmental variables, which is especially important for critical applications like bridge decks or airport runways.
Can automation systems be retrofitted to existing concrete batch plants?
Yes, many automation solutions are retrofittable. Existing mixers can be upgraded with PLC controls, load cells, and sensor integration without complete replacement. However, compatibility depends on equipment age and design. Modern ready mix concrete production facilities benefit most from integrated systems, but retrofitting older concrete batch plant capacity equipment is feasible and often cost-effective compared to purchasing new machinery.